Industry Whitepaper
Navigating China Wholesale Hotel Minibar Procurement: Strategic Insights for B2B Buyers
In the global hospitality sector, guest room electronics represent both a critical customer touchpoint and a significant operational expenditure. Selecting a certified China wholesale hotel minibar manufacturer & factory is no longer merely a pricing decision; it is an integrated engineering choice that directly impacts acoustic comfort, energy management overhead, lifecycle maintenance, and brand consistency.
Modern luxury hotel operators—from global chains to high-end boutique properties—demand in-room appliances engineered specifically for heavy commercial cycles. Consumer-grade mini-refrigerators fail rapidly in hotel settings due to inadequate ventilation design, noisy compressor cycles, and high energy draw. B2B procurement officers, hotel architects, and interior designers must look toward contract-grade OEM/ODM factories capable of matching brand design intent while complying with stringent electrical, thermal, and environmental compliance frameworks worldwide.
Information Gain Insight: Unlike residential compact fridges that operate around 38–45 dB(A), contract-grade hotel minibars using absorption or thermo-electric Peltier technology achieve absolute zero-noise (0 dB) or ultra-low noise (<22 dB), eliminating guest sleep disruption while reducing facility kilowatt-hour usage by up to 35% through modern intelligent thermostat sensors.
Why Source Hotel Minibars & In-Room Amenities Directly from China Factories?
China remains the undisputed epicenter of advanced cooling component fabrication, precision sheet metal stamping, smart thermostat PCB assembly, and architectural lighting integration. By engaging directly with established manufacturing partners in China, procurement teams gain distinctive strategic advantages:
- Unrivaled Cost-to-Performance Ratio: Vertically integrated factories control everything from coil bending and cabinet foamed-in-place polyurethane insulation to automated final testing lines, reducing unit costs by 25–40% compared to Western assembly plants.
- End-to-End Architectural Customization: Custom door panel matching (solid wood veneers, tinted tempered glass, mirrored surfaces, sliding track mounts), dimension adjustments, and customized handle-less designs designed to slip effortlessly into millwork cabinetry.
- Strict Compliance & Global Certifications: World-class Chinese contract factories manufacture fully in compliance with CE, RoHS, UL, ETL, CB, and ISO9001 standards, ensuring hassle-free customs clearance and municipal building code compliance.
Strategic Horizon
Future Procurement Trends in Hospitality Refrigeration & Hardware (2025–2030)
As hotel asset managers and procurement firms plan upcoming turnkeys and brand refresh cycles, several macro technical trends are redefining what makes a minibar factory a viable long-term manufacturing partner:
1. IoT Smart Connectivity & Automated Billing Integration
The traditional manual minibar audit—where housekeeping staff inspects room fridges daily—is rapidly disappearing. Next-generation minibars manufactured in China feature integrated Zigbee, Wi-Fi, or Bluetooth Low Energy (BLE) sensor arrays. Infrared door sensors and weight-sensing shelves automatically transmit consumption data to the property management system (PMS) in real-time, instantly posting charges to the guest's folio while optimizing restock routes for hotel staff.
2. Sustainability, R600a & Zero-ODP Refrigerants
Global environmental mandates (such as the EU F-Gas Regulation and US EPA SNAP guidelines) are driving the phase-out of legacy refrigerants. Modern China wholesale factories have re-engineered their production lines exclusively for eco-friendly hydrocarbon refrigerants like R600a (isobutane) and cyclopentane blowing agents. These materials feature zero Ozone Depletion Potential (ODP) and negligible Global Warming Potential (GWP), aligning with corporate ESG targets.
3. Architectural Cohesion & Integrated Lighting Hardware
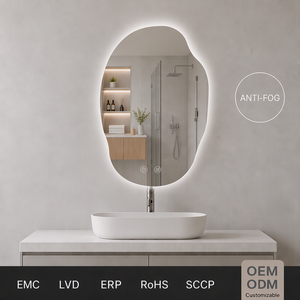
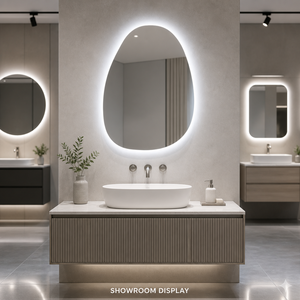
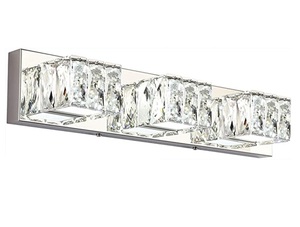
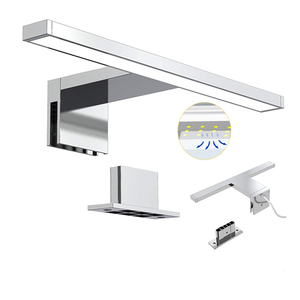
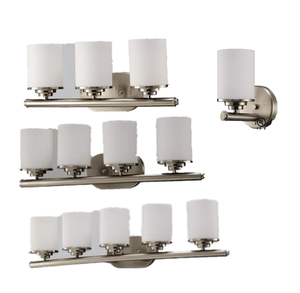
Modern guestroom layouts demand visual integration. Rather than placing a standalone black box in the corner, designers specify minibars with glass doors featuring triple-glazed anti-fog heated glass, customized interior LED light guides (matching the 2700K–3000K warm ambient room temperature), and surrounding wall sconces or illuminated vanity mirrors that use shared architectural metals (such as brushed nickel, statuary bronze, or prismatic gold).
100,000 Sq Ft Advanced Production Base
Our centralized production infrastructure handles end-to-end manufacturing: automated metal sheet spinning, CNC laser cutting, robotic welding, polyurethane foaming, vacuum liquid charging, electrical safety testing, and automated shade and fixture assembly under one roof. In-house manufacturing guarantees total quality control, rapid prototyping, and reliable delivery timelines for high-volume contract projects.
Contract-Grade Durability & Safety Testing
Every commercial unit undergoes rigorous 100% electrical high-pot testing, thermal stability testing in high-ambient humidity chambers, and drop testing for export packaging. Finishes, metal platings, and wood veneers are chemical-resistance tested to withstand aggressive daily housekeeping disinfections without peeling, tarnishing, or corroding.
Flexible MOQs & Customization Support
We understand project flexibility is crucial. While standard volume production supports major hotel franchise rollouts, our flexible manufacturing lines accommodate smaller boutique programs, starting from single-piece sample approvals for mock-up rooms to scalable phased releases tailored to contractor construction schedules.
Global Logistics & Dual-Coast Distribution
With integrated logistics networks across major international ports and distribution support on both East and West coasts, we streamline customs documentation, tariff classification, container optimization, and floor-by-floor jobsite delivery so installation crews can work efficiently without delays.
What is the difference between absorption and compressor hotel minibars?
Absorption minibars operate using a heat-driven cooling cycle with no moving parts or motor compressors, rendering them 100% silent (0 dB). They are ideal for high-end luxury guest rooms where complete acoustic silence is mandated. Compressor minibars use a mechanical pump; while slightly louder (28-35 dB), modern inverter compressor minibars consume less power and cool faster. Most luxury hotels prefer absorption or specialized thermo-electric units for guest rooms.
Can minibars be customized to match custom hotel joinery and furniture?
Yes. As a direct OEM/ODM manufacturer, we offer complete structural and aesthetic customization. This includes custom cabinet dimensions, interchangeable front door panels (solid wood veneer, brushed stainless steel, frosted or clear glass), custom door handles, internal sliding hinges for integrated cabinetry doors, and specific color-temperature LED interior lighting.
What are the typical lead times for wholesale factory orders?
Standard prototype and mock-up samples are typically produced within 7 to 14 days. Full production orders generally require 25 to 35 days depending on total order volume, level of customization, and current factory line capacity. Sea freight delivery timelines vary by destination port, and expedited air transport can be arranged for urgency.
How do you handle voltage, plug, and electrical compliance for different export markets?
All products are engineered to meet regional electrical standards: 110-120V / 60Hz (US/North America), 220-240V / 50Hz (Europe, Asia, Middle East, UK), or universal dual-voltage configurations. Units are shipped with regional plugs (US, EU, UK, AU) and carry international safety certifications including CE, RoHS, UL, ETL, and CB certificates.
What are the minimum order quantities (MOQ) for custom B2B projects?
Minimum order quantities depend on the product category and level of custom tooling required. Standard catalog models can often be ordered in batches as low as 12 to 25 units. Fully custom engineered dimensions or specialized finishes typically start at 50 to 100 units. Sample units for hotel mock-up rooms are always supported.
How is proper thermal ventilation ensured when minibars are built into cabinetry?
Proper airflow is critical for minibar cooling efficiency and unit longevity. We provide detailed installation guidelines and engineered cabinet ventilation templates. A minimum ventilation channel of 200 cm² at both the bottom air intake and top air outlet is required to ensure heat escapes freely from the rear condenser coils.